



A bio-based thickener can meet its viscosity specification and still change filling behavior, suspension stability, or product texture. Batch consistency therefore means more than repeated compliance with a certificate of analysis (CoA): it means reproducible performance under the conditions that matter in the finished formulation.
The strongest qualification evidence combines independently manufactured lots, a reproducible preparation and measurement method, and application tests with predefined acceptance limits. A single approved sample establishes feasibility. It does not establish that routine deliveries will behave the same way.
Define consistency in terms of the process, not just the powder
Before comparing manufacturers, identify which material properties could disrupt production or finished-product quality. For xanthan gum in a suspension, low-shear behavior may matter more than viscosity at the supplier’s release-test speed. For a starch-based thickener, the heating profile and resistance to processing shear may determine performance. For pectin or alginate, gelation behavior and sensitivity to ions can be decisive.
These differences make a universal “batch consistency” specification unreliable. The acceptance criteria must reflect the specific grade, formulation, and manufacturing process.
Separate non-negotiable safety and identity requirements from functional performance limits. A lot with excellent rheology cannot compensate for an unacceptable microbiological result, incorrect identity, or a restricted contaminant above the applicable limit.
Make the test method reproducible before judging the supplier
A viscosity value without preparation and measurement conditions is weak evidence. Hydrocolloid solutions can respond to concentration, water chemistry, temperature, hydration time, and shear history. Differences between laboratories can therefore resemble batch variation even when the material itself is unchanged.
Obtain the manufacturer’s complete method, not just the instrument name. Establish agreement on:
- Concentration basis: percentage by mass or another clearly defined basis, with explicit treatment of moisture and active content where relevant.
- Preparation medium: water quality, pH, salts, buffering agents, and other ingredients present during hydration.
- Dispersion procedure: addition order, feed rate, mixer geometry, vessel dimensions, mixing speed, duration, and batch size.
- Conditioning: hydration endpoint, temperature equilibration, resting time, and any deaeration step.
- Measurement settings: instrument geometry or spindle, speed or shear rate, reading time, temperature, and pre-shear sequence.
For materials that shear-thin, spindle speed alone is not a transferable shear-rate specification across different geometries. Likewise, using the same mixer speed in different vessels does not reproduce the same dispersion conditions. A method intended for multiple laboratories needs enough detail to reproduce the preparation, not merely the final reading.
Use both the supplier’s release method and an application-relevant method when they answer different questions. The release method supports comparison with historical production data; the application method establishes whether that variation matters in use.
A split-sample comparison helps expose laboratory bias. Both laboratories should test portions of the same homogenized sample, with independent preparations and recorded deviations. Resolve a persistent offset before tightening acceptance limits or rejecting lots.
Ask for independent production lots, not repeated samples of one batch
Qualification samples should represent separate manufacturing events. Several containers from one lot can reveal within-lot variation, but they cannot demonstrate lot-to-lot consistency. Similarly, repeated instrument readings from one prepared solution measure reading repeatability, not manufacturing reproducibility.
An initial screen using three independent lots can reveal obvious differences, but it provides limited evidence about long-term variability. Increase coverage according to application sensitivity, manufacturing risk, and available production history. Include different raw-material receipts, production campaigns, or manufacturing lines where those are relevant sources of variation.
Request the following evidence for the exact commercial grade and manufacturing site:
- Lot-level numerical release results over a defined historical period, rather than only “pass” statements or selected CoAs.
- Identification of the production line, manufacturing date, and relevant raw-material or intermediate-lot links.
- Sampling procedures showing how the release sample represents the finished batch.
- Details of blending, reprocessing, or adjustment used to bring material within specification.
- Available deviation, out-of-specification, and complaint investigations relevant to functional consistency.
Blending is not inherently a weakness; it can be a controlled way to normalize natural feedstock variation. The important questions are whether the blend is homogeneous, traceable, and functionally equivalent. A final viscosity result alone does not establish those points.
Use rheological fingerprints where one-point viscosity is insufficient
Two lots can have the same viscosity at one measurement condition and different flow behavior elsewhere. A flow curve across the application’s relevant shear range can expose this difference. It is particularly useful when a material must provide structure during storage while remaining pumpable during processing.
Time-dependent behavior deserves separate attention. Compare viscosity development during hydration and recovery after a defined shear treatment. A lot that eventually reaches the target viscosity may still cause problems if production transfers the mixture before hydration is complete.
For gel-forming or structured systems, oscillatory measurements can provide useful information about elastic and viscous behavior. The method must establish suitable test conditions, including the linear viscoelastic region where applicable. Yield-stress results also depend on method and sample history; values from different protocols should not be treated as directly interchangeable.
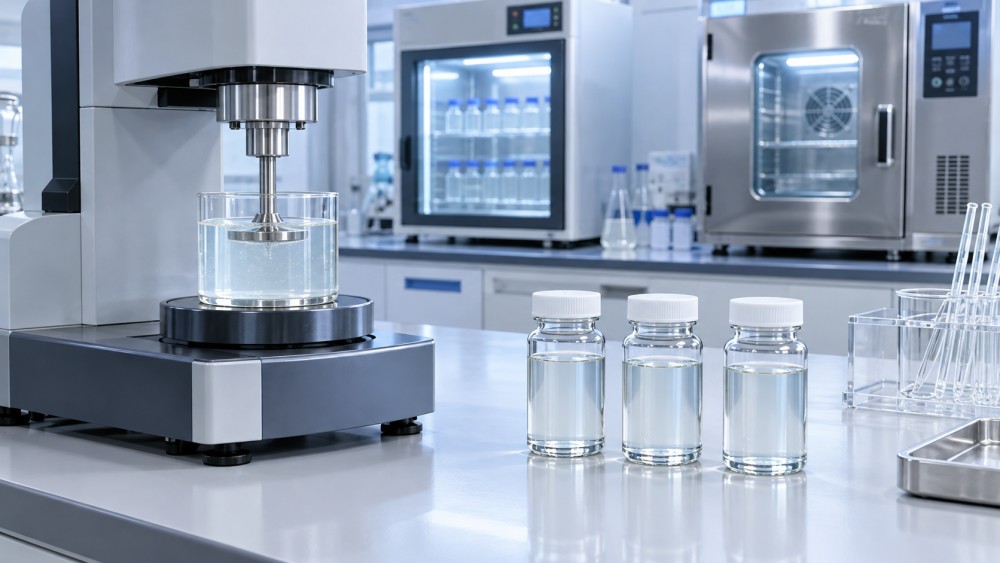
Keep the qualification panel focused. Select measurements tied to a plausible failure mechanism rather than collecting every available rheological parameter. A fuller fingerprint can support initial approval and investigations, while a smaller validated set may be sufficient for routine incoming control.
Separate real batch variation from test noise
Independent sample preparations are essential. Re-reading the same cup can demonstrate instrument stability while missing variation caused by weighing, dispersion, or hydration. Include preparation replicates, and use a stable reference material to monitor laboratory drift where practical.
Review individual results in manufacturing-date order, not just as an overall average. A satisfactory average can conceal a steady shift, alternating production-line effects, or a widening spread. Compare variation within lots, between lots, and between laboratories before attributing the full difference to manufacturing.
Standard deviation and coefficient of variation can summarize suitable numerical results, but they are not acceptance criteria by themselves. The coefficient of variation becomes difficult to interpret when the mean is close to zero. Process capability indices are meaningful only when the measurement system is adequate, the process is sufficiently stable, and the statistical assumptions are appropriate.
Distinguish specification limits from statistical control limits. Specifications define acceptable material; control limits describe observed process behavior. A process can be statistically stable but unable to meet the application’s needs, or remain within a broad specification while undergoing a meaningful shift.
Check whether raw-material controls explain the observed performance
“Bio-based” describes origin, not uniformity. Plant-derived gums, fermentation-derived polysaccharides, cellulose derivatives, and modified starches have different sources of variability. Traceability should follow the factors relevant to the material rather than stop at a feedstock name.
For a plant-derived hydrocolloid, relevant controls may include botanical identity, source, extraction conditions, and purification. For a fermentation-derived material, examine control of fermentation inputs, recovery, and downstream processing. For chemically modified bio-based polymers, substitution characteristics and process control can be important to functional reproducibility.
Supporting measurements should help explain performance. Moisture affects the amount of dry material delivered at a fixed as-received dosage. Particle-size distribution can affect dispersion and hydration. Ash or residual salts may influence ion-sensitive systems. Molecular characteristics can matter where processing changes chain length or substitution.
Test material as it will actually be dosed. If production uses an as-received mass basis, dry-basis comparisons alone may hide operational variation. Dry-basis results can still help determine whether an apparent difference comes from moisture or intrinsic thickening performance.
Treat microbiology, storage, and packaging as separate qualification gates
Microbiological acceptance must match the intended use and applicable requirements. Request organism-specific requirements where relevant, test methods, sample quantities, and the basis for release. A total count alone does not answer every safety question, and passing a powder release test does not demonstrate preservation of the finished formulation.
Review how the manufacturer prevents contamination during drying, milling, blending, and packing. For dry powders, moisture and water activity provide different information: moisture measures water content, while water activity relates to water availability. Neither replaces appropriate microbiological testing.
Compare fresh material with retained or aged samples when storage could change hydration, odor, color, or performance. Packaging suitability, seal integrity, humidity exposure, and transport conditions belong in that assessment. An accelerated study supports shelf-life judgment only when its conditions and failure mechanisms are relevant to real storage.
Make the qualification decision in the actual formulation
Water-based tests isolate material differences, but the formulation determines their consequences. Test qualified lots in a representative matrix containing the relevant salts, acids, sugars, surfactants, proteins, or other interacting ingredients. Reproduce addition order and the thermal and shear sequence as closely as practical.
Start with a fixed dosage and fixed process. Adjusting each lot until the final viscosity matches can conceal inconsistency. If routine dosage adjustment is acceptable, assess it separately and define its limits, measurement requirements, and effects on other product attributes.
Challenge realistic operating boundaries rather than arbitrary extremes. Compare performance near permitted pH or temperature limits, at the shortest allowed hydration time, or after the most demanding approved shear exposure. A supplier whose material works only at the center of the operating window offers less manufacturing tolerance than one that remains acceptable across it.
Set acceptance limits before reviewing the qualification results. Base them on product and process requirements, supported by testing, rather than adopting the manufacturer’s full specification range without checking its suitability.
Approval should include control of future changes
A capable bio-based thickener manufacturer should be able to explain not only why current lots are consistent, but how that consistency will be maintained. Define notification requirements for changes to raw-material sources, manufacturing sites, equipment, processing conditions, blending practices, test methods, and packaging where these could affect performance.
Link significant changes to a documented impact assessment and, where necessary, comparative testing or requalification. Establish how disputed results will be investigated, which method governs release, and how retained samples will be used.
Approve the specific grade, site, and manufacturing route supported by the evidence—not the supplier’s entire portfolio. Where historical coverage is limited but application results are acceptable, conditional approval with enhanced incoming testing is more defensible than treating a small sample set as proof of long-term control. The decisive evidence is a controlled relationship between manufacturing variation and acceptable application performance.
Related News
- How to choose food hydrocolloids for gluten-free breadNov 03, 2026Food Rheology Expert
- How to choose food-grade hydrocolloid ingredients for stable saucesOct 30, 2026Food Rheology Expert
- How to assess a bio-based thickener manufacturer's batch consistencyOct 16, 2026Food Rheology Expert
- Verifying halal status of hydrocolloid ingredients in the Middle EastOct 15, 2026Food Rheology Expert
Related News
- 00
0000-00
Wissen Research: Global Cosmetics Market to Reach $497.2 Billion by 2031 - 00
0000-00
Can biomimetic peptides improve skin firmness? - 00
0000-00
China Records 543 New Cosmetic Ingredients, Including 167 in 2026 - 00
0000-00
How to check a fragrance raw material specification for IFRA compliance - 00
0000-00
Australia and New Zealand Weigh Wider Steviol Glycoside Use in Griddle Products
Food Rheology Expert
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.